Airflow Conveying of Phenolic Resin Powder: An Efficient and Eco-Friendly Material Handling Solution
Phenolic resin powder, widely used in various industrial applications such as molding, coating, and composite manufacturing, presents unique challenges during material handling. Traditional methods like mechanical conveying often suffer from issues like dust generation, equipment wear, and inefficiencies. To address these challenges, modern industrial practices increasingly adopt airflow conveying systems, which offer a more efficient, safer, and environmentally friendly approach to transporting phenolic resin powder.
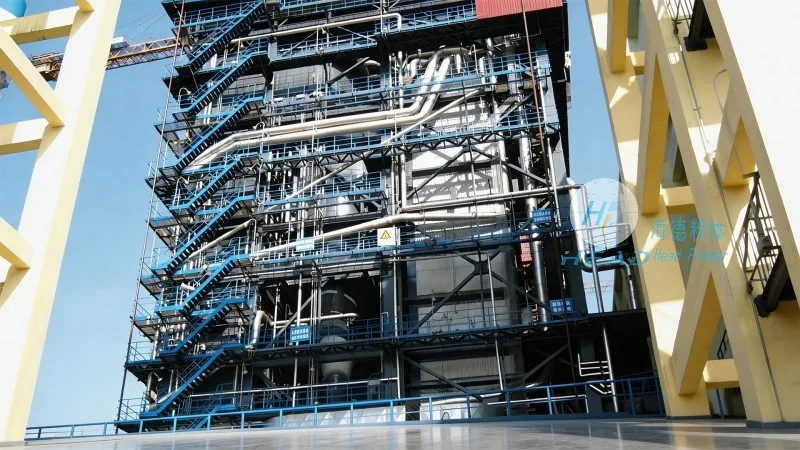
HeadPowder, a leading provider of specialized material handling solutions, specializes in developing and implementing advanced airflow conveying systems tailored for phenolic resin powder applications. The company, Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China, and has a strong reputation for delivering high-quality, reliable solutions that meet the unique needs of its clients.
Key Advantages of Airflow Conveying for Phenolic Resin Powder
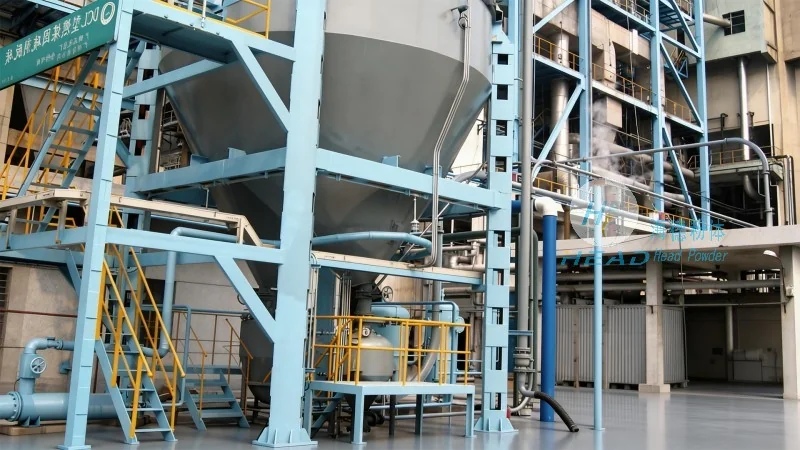
One of the primary benefits of using airflow conveying for phenolic resin powder is its ability to minimize dust and airborne particles. Unlike mechanical systems that may generate significant dust, air-based conveying uses a controlled airflow to transport the powder, significantly reducing the risk of respiratory issues and contamination. This not only improves worker health and safety but also maintains the purity of the phenolic resin powder, which is critical for high-quality end products.
Efficiency is another critical advantage. Airflow conveying systems can handle high volumes of phenolic resin powder with minimal energy consumption compared to traditional methods. The system's design, including proper ductwork, air velocity control, and material feed mechanisms, ensures consistent and reliable material flow, reducing downtime and increasing overall production throughput. HeadPowder's engineers carefully design each system to match the specific characteristics of the phenolic resin powder, such as particle size, density, and moisture content, to achieve optimal performance.
Environmental and Operational Benefits
From an environmental perspective, airflow conveying of phenolic resin powder is a highly sustainable solution. By reducing dust emissions and minimizing the need for additional cleaning or maintenance, the system lowers the environmental footprint of industrial operations. This aligns with global sustainability goals and helps companies meet regulatory requirements for air quality and waste management.
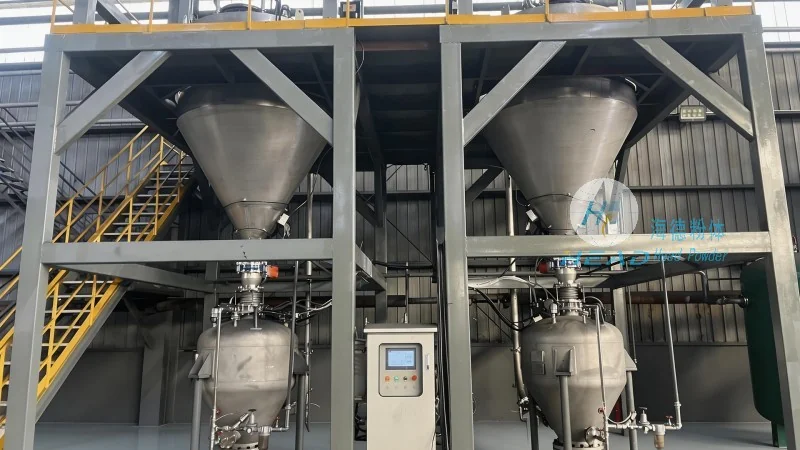
Operational costs are also reduced through the efficiency gains and reduced maintenance needs. The use of air-based systems eliminates the need for heavy machinery and frequent part replacements, which are common in mechanical conveying systems. Additionally, the reduced risk of product contamination and equipment damage further contributes to long-term cost savings.
HeadPowder's Comprehensive Solutions
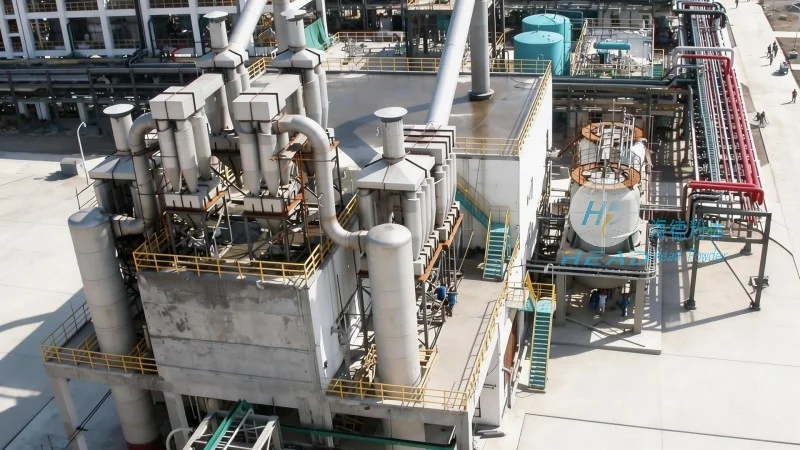
HeadPowder offers a comprehensive range of services to support the implementation of airflow conveying systems for phenolic resin powder. From initial system design and engineering to installation, commissioning, and ongoing maintenance, the company provides end-to-end solutions tailored to each client's specific needs. The company's team of experienced engineers works closely with clients to understand their production requirements, material characteristics, and operational constraints, ensuring that the final system is optimized for maximum efficiency and minimal environmental impact.
HeadPowder's commitment to quality and innovation is reflected in its use of advanced materials and technologies in the construction of conveying components. The company selects high-quality materials that are resistant to corrosion and wear, ensuring the longevity of the system. Additionally, the company invests in research and development to continuously improve its systems, incorporating the latest advancements in airflow dynamics and material handling to stay ahead of industry trends.
Conclusion
For industries dealing with phenolic resin powder, airflow conveying represents a significant step forward in material handling technology. By combining efficiency, safety, and environmental responsibility, these systems offer a superior alternative to traditional methods. HeadPowder, with its expertise and comprehensive solutions, plays a crucial role in helping companies adopt and benefit from this advanced technology, ensuring their operations remain competitive and sustainable in the long term.