Common Coal Ash Particle Conveying Methods: Advantages and Features of HeadPowder's Pneumatic Conveying System
Efficient and reliable transport of coal ash particles is a critical requirement in industrial operations, particularly in power generation and waste management sectors. Coal ash, a byproduct of coal combustion, poses unique challenges due to its fine particle size, abrasive nature, and potential environmental impact. Traditional conveying methods, such as belt conveyors and screw conveyors, often struggle to meet these demands, leading to operational inefficiencies and safety concerns. This article explores common coal ash particle conveying methods and highlights the advantages of HeadPowder's pneumatic conveying system, a cutting-edge solution designed to address these challenges effectively.
Traditional Conveying Methods and Their Limitations
Historically, industries have relied on mechanical conveyors like belt conveyors, screw conveyors, and bucket elevators to transport coal ash. While these methods are widely used, they come with significant drawbacks. Belt conveyors, for instance, are susceptible to wear from abrasive ash particles, leading to frequent maintenance and downtime. Screw conveyors, though compact, can cause blockages and require regular cleaning, especially with fine ash. Bucket elevators, another traditional option, have moving parts that increase the risk of accidents and are less effective for handling very fine particles. Additionally, all these mechanical systems generate dust, which poses health hazards and requires extensive dust control measures. These limitations highlight the need for more advanced and efficient conveying technologies.
HeadPowder's Pneumatic Conveying System: Core Advantages
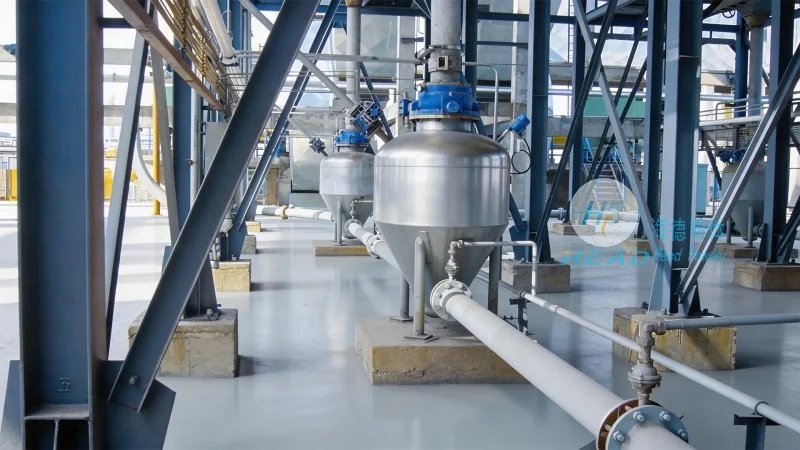
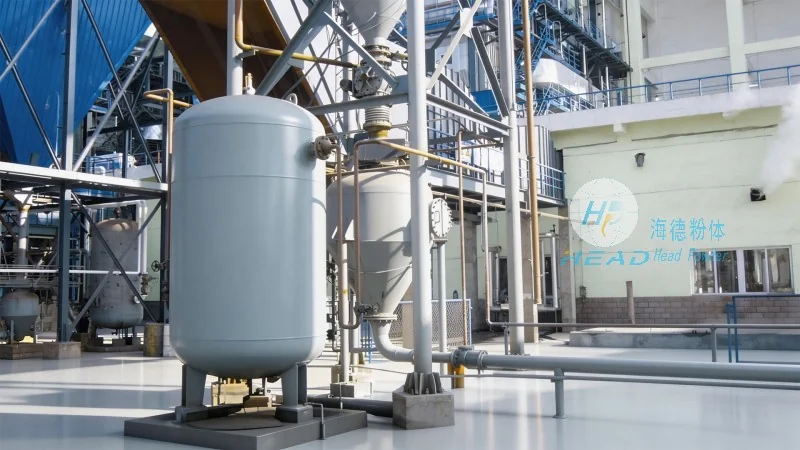
HeadPowder, a leading provider of material handling solutions, offers a pneumatic conveying system specifically tailored for coal ash particles. This system represents a significant advancement over traditional methods, offering several key advantages. First, it eliminates the need for mechanical components in contact with the ash, reducing wear and tear and minimizing maintenance requirements. Second, the enclosed system ensures dust is contained, enhancing workplace safety and compliance with environmental regulations. Third, the flexibility of pneumatic conveying allows for horizontal, vertical, or complex path layouts, making it suitable for diverse industrial settings. Finally, the system's ability to handle both fine and coarse ash particles with equal efficiency makes it a versatile solution for various applications.
Key Features of the Pneumatic Conveying Technology
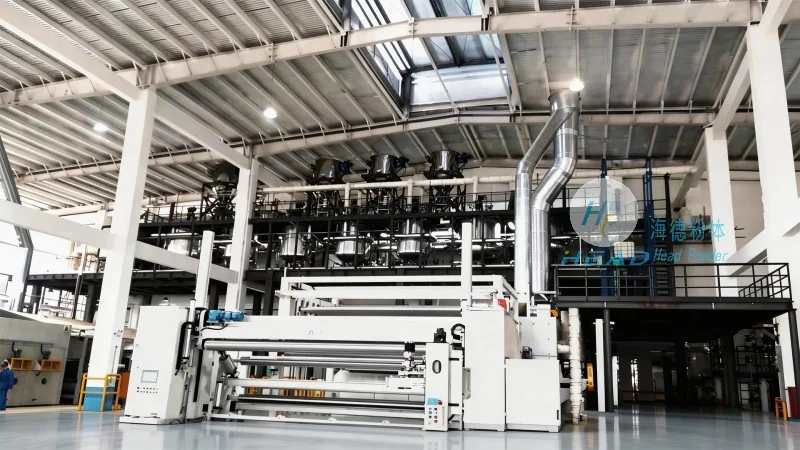
The pneumatic conveying system developed by HeadPowder incorporates several innovative features that enhance its performance and reliability. The system operates on either positive or negative pressure, depending on the specific application and layout requirements. Positive pressure systems use air to push the ash particles through the pipeline, while negative pressure systems draw the particles into the system using suction. This dual capability allows for flexible installation, even in challenging environments. The material handling capacity of the system is designed to accommodate high volumes of coal ash, with adjustable flow rates to match production needs. Additionally, the system's robust construction, including corrosion-resistant materials and advanced sealing mechanisms, ensures long-term durability and minimal downtime. The use of high-efficiency air filters and dust collection systems further enhances the system's environmental performance, reducing emissions and maintaining clean operation.
Application Scenarios and Operational Benefits
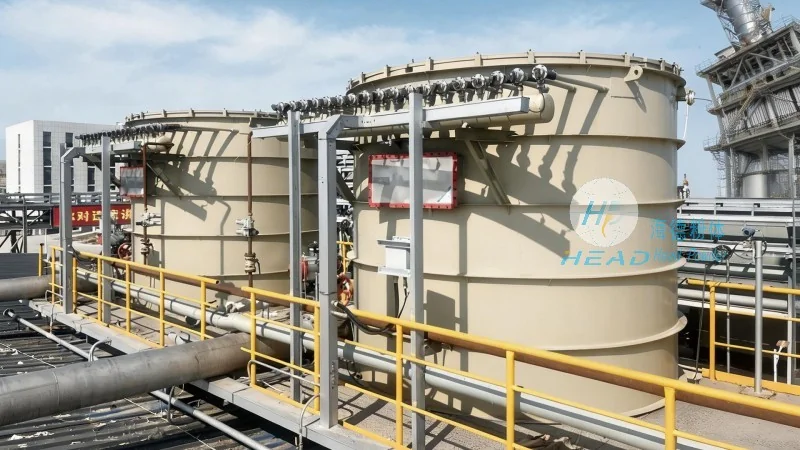
HeadPowder's pneumatic conveying system is widely applied in various industrial scenarios, including power plants, coal-fired facilities, and waste treatment centers. In power plants, the system efficiently transports coal ash from boilers to storage silos or disposal sites, ensuring smooth operation and minimizing disruptions. In waste management facilities, it helps in the processing and recycling of coal ash, contributing to sustainable waste management practices. The operational benefits of this system are evident in improved safety, reduced maintenance costs, and enhanced environmental compliance. By eliminating manual handling and enclosed transport, the system reduces the risk of occupational hazards and ensures that ash is handled in a controlled manner. Furthermore, the system's ability to handle long distances and complex layouts makes it ideal for large-scale industrial operations, where traditional conveyors may be impractical.
Conclusion and Company Overview
In conclusion, the transition from traditional mechanical conveying methods to advanced pneumatic systems like HeadPowder's is essential for efficient and safe coal ash particle transport. The advantages of this technology, including reduced maintenance, enhanced safety, and improved environmental performance, make it a superior choice for modern industrial applications. Shandong HeadPowder Engineering Co., Ltd., based in China, has established itself as a leader in this field, providing innovative solutions that meet the evolving needs of the industry. With a focus on quality, reliability, and customer satisfaction, HeadPowder continues to advance material handling technologies, ensuring that coal ash is managed effectively and responsibly. The company's commitment to research and development ensures that its products remain at the forefront of industry standards, offering long-term value to its clients.