Common Cement Fly Ash Conveying Methods: Advantages and Features of HeadPowder's Pneumatic Conveying System
When it comes to transporting cement and fly ash, selecting the right conveying method is crucial for efficiency, cost-effectiveness, and operational safety. Various technologies are available, each with its own set of advantages and limitations. This article explores common cement fly ash conveying methods and highlights the superior features of HeadPowder's pneumatic conveying system.
Overview of Traditional Cement Fly Ash Conveying Methods
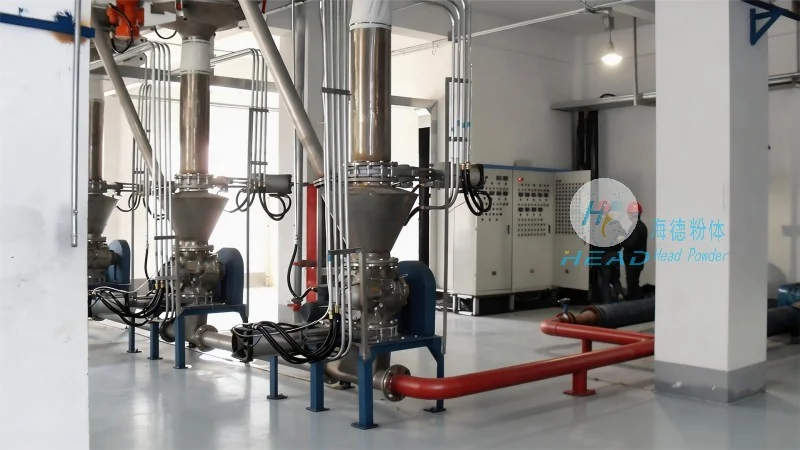
Traditional conveying methods for cement and fly ash often include mechanical systems such as belt conveyors, screw conveyors, and bucket elevators. These systems have been widely used in the industry for decades. Belt conveyors, for instance, are effective for horizontal or slightly inclined transport but may face challenges with material buildup, especially with fine powders like fly ash. Screw conveyors are suitable for moderate distances and can handle bulk materials but are prone to blockages and wear from abrasive materials. Bucket elevators are ideal for vertical transport but require regular maintenance to prevent mechanical failures.
Advantages of Pneumatic Conveying for Cement Fly Ash
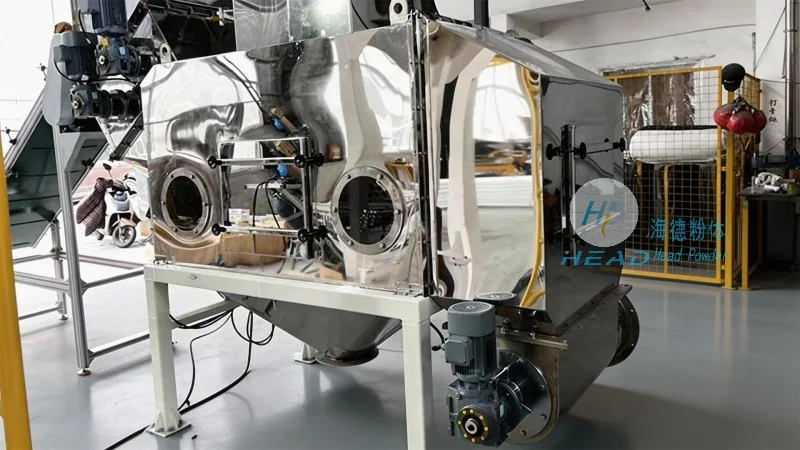
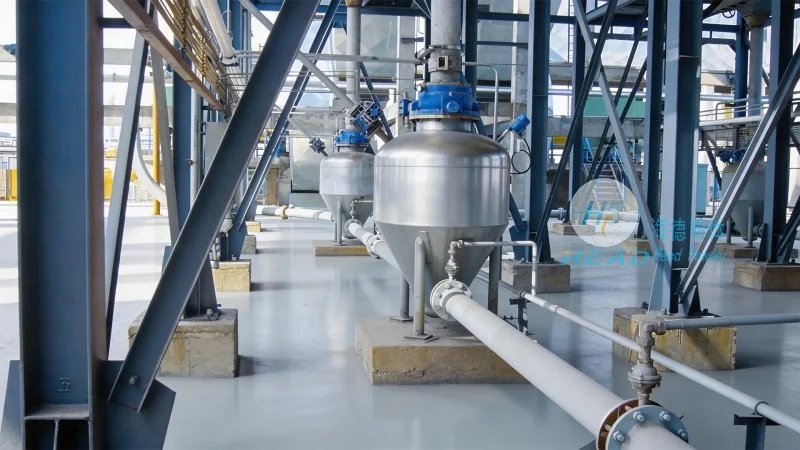
Pneumatic conveying, also known as air-powered conveying, offers a more flexible and efficient solution for transporting cement and fly ash. Unlike mechanical systems, it eliminates the need for moving parts in contact with the material, reducing wear and maintenance costs. The system uses compressed air to move the material through a pipeline, allowing for both positive and negative pressure operation. This flexibility enables the system to handle varying material characteristics and transport distances without significant modifications.
Key Features of HeadPowder's Pneumatic Conveying System
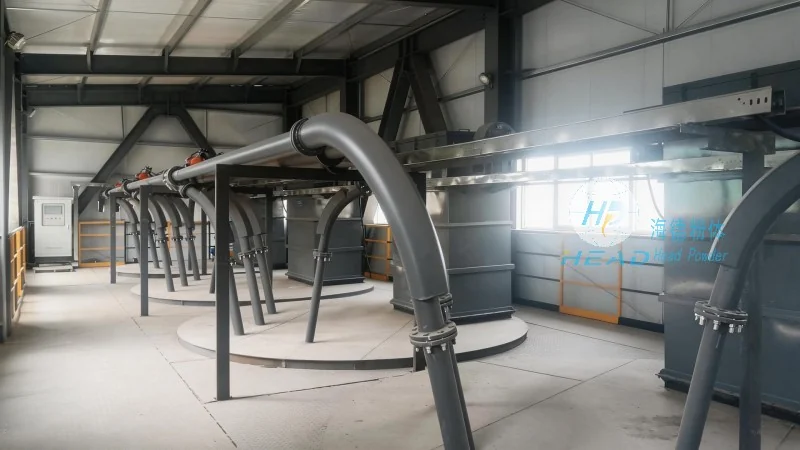
HeadPowder, a leading provider of industrial conveying solutions, offers advanced pneumatic conveying systems tailored for cement and fly ash applications. The company's system incorporates several key features that enhance performance and reliability. One of the primary advantages is the use of high-efficiency air compressors and filtration systems, which ensure consistent air quality and reduce the risk of material contamination. The pipeline design incorporates smooth, corrosion-resistant materials, minimizing friction and preventing material degradation during transport. Additionally, the system includes intelligent control panels that allow for real-time monitoring and adjustment of conveying parameters, optimizing energy usage and operational efficiency.
Operational Benefits and Cost Efficiency
The implementation of HeadPowder's pneumatic conveying system provides several operational benefits. By eliminating the need for multiple transfer points and mechanical components, the system reduces downtime and maintenance requirements, leading to lower overall operational costs. The ability to transport materials over longer distances with fewer intermediate points also improves process flow and reduces the risk of material spillage or contamination. Furthermore, the system's energy-efficient design minimizes electricity consumption, contributing to lower operational expenses and a smaller environmental footprint.
Customization and Scalability
HeadPowder understands that each industrial application has unique requirements. The company offers customized pneumatic conveying solutions that can be scaled to meet specific production needs. Whether for small-scale operations or large industrial facilities, the system can be adjusted to handle varying material volumes and transport distances. The modular design allows for easy expansion or modification as production needs evolve, ensuring long-term investment value.
Conclusion
In conclusion, while traditional mechanical conveying methods have their place in the industry, pneumatic conveying offers a more advanced and efficient solution for transporting cement and fly ash. HeadPowder's pneumatic conveying system stands out with its superior features, including reduced maintenance, flexible operation, and energy efficiency. By choosing HeadPowder's solution, industrial facilities can enhance their operational performance, reduce costs, and improve overall productivity. For those seeking reliable and effective cement fly ash conveying solutions, HeadPowder provides a trusted and innovative approach to meet their needs.