Conveying Methods for Potassium Carbonate Fertilizer: An Overview of the Advantages and Features of
When it comes to transporting potassium carbonate fertilizer, selecting the right conveying method is crucial for ensuring efficiency, safety, and cost-effectiveness in industrial operations. Among the various options available, pneumatic conveying stands out as a highly effective solution, particularly for handling potassium carbonate, a key component in modern agricultural and industrial applications. This article provides an in-depth look at the different conveying methods for potassium carbonate fertilizer and highlights the unique advantages and characteristics of pneumatic conveying systems.
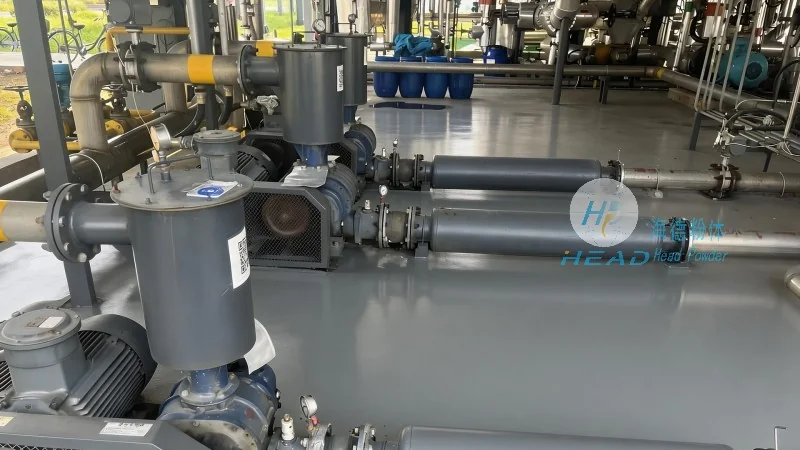
Understanding the Conveying Methods for Potassium Carbonate Fertilizer
Potassium carbonate fertilizer, often used in agriculture and chemical manufacturing, requires specialized handling due to its granular or powdered nature. Traditional methods like belt conveyors or screw conveyors may struggle with dust generation, material segregation, and operational inefficiencies when dealing with this type of fertilizer. In contrast, pneumatic conveying offers a more controlled and efficient approach, leveraging air pressure to move the material through a system of pipes and ducts.
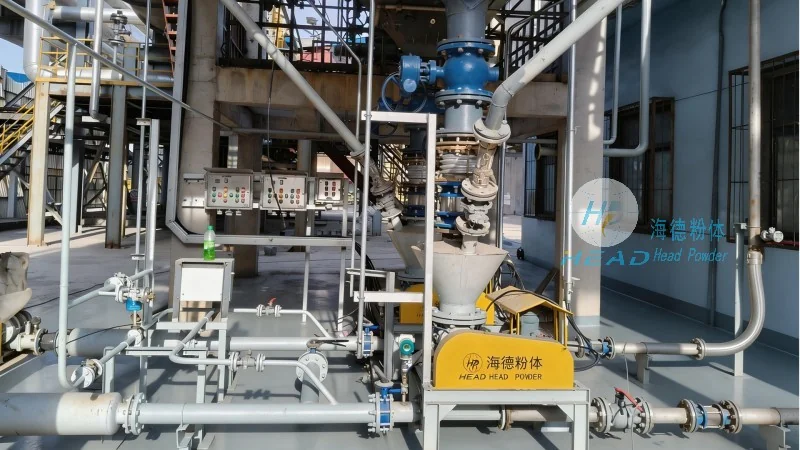
The Advantages of Pneumatic Conveying for Potassium Carbonate Fertilizer
One of the primary advantages of pneumatic conveying is its ability to handle the dust and fine particles associated with potassium carbonate fertilizer without the need for additional dust suppression equipment. The system operates by creating a pressure differential, either through positive or negative pressure, to draw or push the material through the pipeline. This method minimizes material loss and contamination, which is critical for maintaining the quality of the fertilizer. Additionally, pneumatic conveying systems can be designed to handle varying flow rates and material characteristics, making them adaptable to different production scales and operational needs.
Key Features of Pneumatic Conveying Systems for Potassium Carbonate
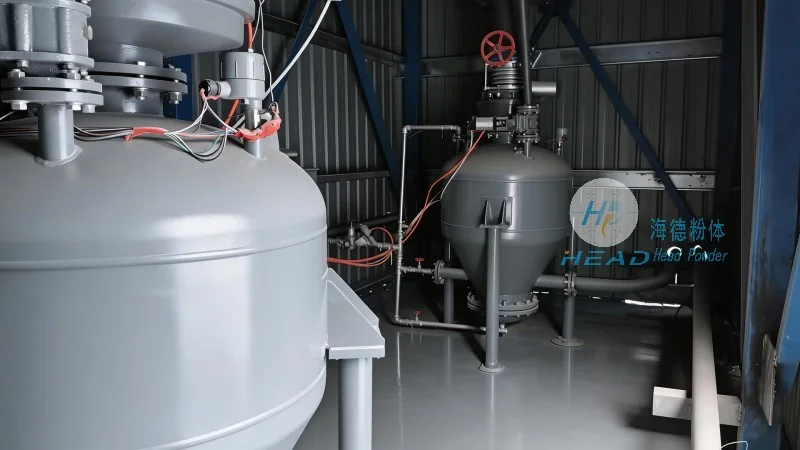
Modern pneumatic conveying systems for potassium carbonate fertilizer are equipped with several features that enhance their performance and reliability. These include: 1. Self-Cleaning Design: The system is designed to prevent material buildup in the pipes, reducing the risk of clogging and ensuring consistent flow. 2. Energy Efficiency: Advanced control systems optimize air usage, reducing energy consumption compared to traditional methods. 3. Modular Construction: Systems can be easily expanded or reconfigured to accommodate changes in production requirements. 4. Low Maintenance: The use of durable materials and robust components minimizes downtime and maintenance costs.
Applications and Operational Benefits
Pneumatic conveying systems are widely used in the processing and distribution of potassium carbonate fertilizer. They are particularly effective in applications where material needs to be moved over long distances or through complex layouts, such as in large-scale fertilizer plants or distribution centers. The ability to transport material in a closed system also helps in maintaining hygiene standards, which is essential for products intended for agricultural use. Furthermore, the system's ability to handle both dry and slightly moist materials makes it versatile for different types of potassium carbonate formulations.
Conclusion and Company Overview
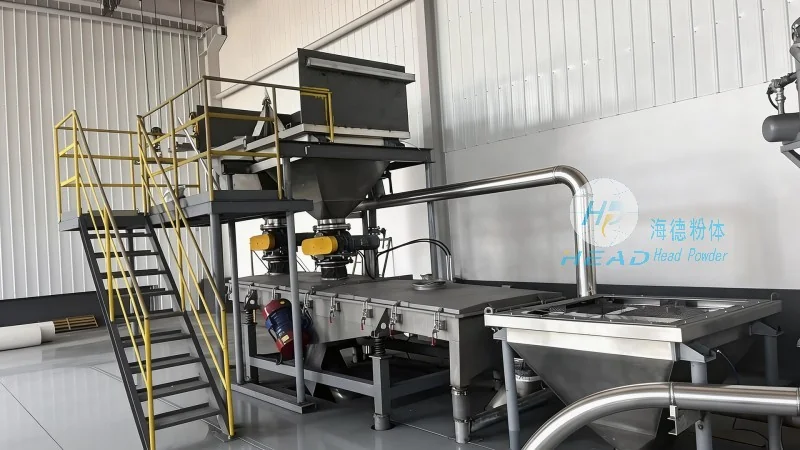
In conclusion, pneumatic conveying represents a superior method for transporting potassium carbonate fertilizer, offering significant advantages in efficiency, safety, and material handling. For businesses looking to optimize their fertilizer processing and distribution operations, investing in a well-designed pneumatic conveying system can lead to improved productivity and cost savings. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in developing and manufacturing advanced pneumatic conveying solutions tailored to the specific needs of potassium carbonate fertilizer applications. With a focus on quality and innovation, the company ensures that its systems meet the highest standards of performance and reliability, helping clients achieve their operational goals effectively.