Common Rice and Flour Conveying Methods: A Comparative Analysis
When it comes to the efficient handling and transportation of rice and flour in industrial settings, selecting the right conveying method is crucial for maintaining product quality, minimizing downtime, and optimizing operational costs. Various technologies are available, each with distinct advantages and applications. This article provides a detailed comparison of common rice and flour conveying methods, highlighting the features, benefits, and ideal use cases for each system.
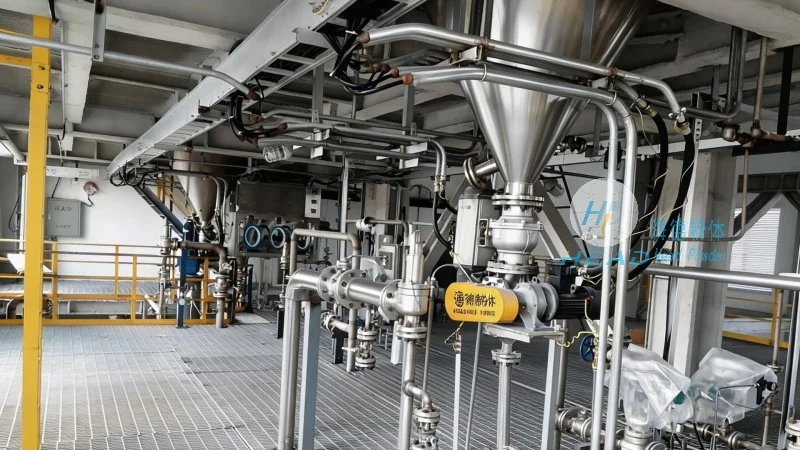
1. Screw Conveyors: The Traditional Choice for Bulk Material Handling
Screw conveyors, also known as auger conveyors, are among the most widely used equipment for transporting rice and flour. These systems consist of a rotating screw (auger) enclosed in a U-shaped or cylindrical housing. As the screw rotates, it pushes material forward through the housing, making them ideal for horizontal or slight incline applications. HeadPowder, a leading manufacturer based in Shandong, China, offers high-quality screw conveyors designed to handle a wide range of grain types and flour consistency. The company’s screw conveyors are engineered with durable materials, such as stainless steel or food-grade plastics, to ensure compliance with sanitary standards and prevent contamination. Key technical specifications include adjustable screw speeds (typically ranging from 10 to 100 RPM) and variable pitch designs to control material flow rate. These conveyors are capable of handling materials with particle sizes from 1 mm to 50 mm, making them suitable for both raw rice and milled flour. The compact design of screw conveyors allows for easy integration into existing processing lines, and their low maintenance requirements reduce operational downtime. HeadPowder’s screw conveyors are equipped with features like variable speed drives and material sensors to enhance control and efficiency. They are particularly suitable for short to medium-distance transport within processing plants, such as moving raw rice from storage silos to milling equipment or conveying flour from grinding mills to packaging lines. The company’s screw conveyors have been tested and approved for use in food processing environments, ensuring safety and compliance with industry regulations.
2. Pneumatic Conveying Systems: Efficient for Dusty and Light Materials
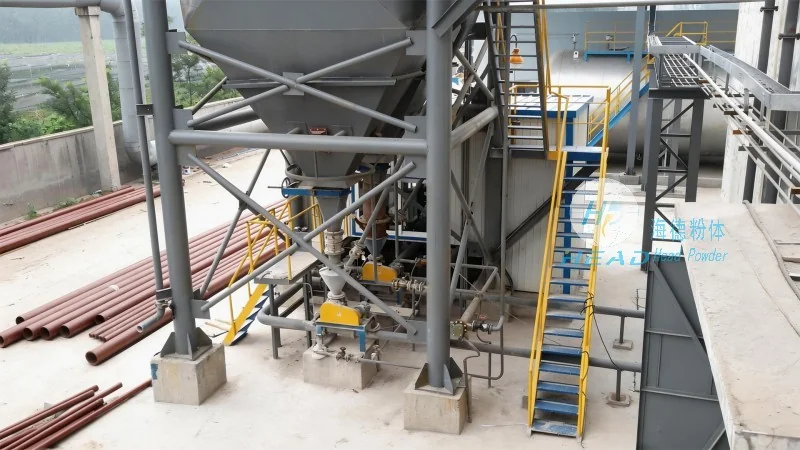
Pneumatic conveying systems use air or gas to transport rice and flour through a network of pipes. These systems are highly effective for handling dusty, light, or fine materials that are prone to segregation or contamination. HeadPowder’s pneumatic conveying solutions are designed with positive displacement blowers or venturi systems, ensuring consistent and controlled material flow. The company’s systems are equipped with features like cyclone separators and filter bags to maintain air quality and prevent material buildup. Pneumatic conveyors offer advantages such as minimal product degradation, easy integration with existing processing lines, and the ability to transport materials over longer distances with fewer transfer points. They are commonly used in applications where hygiene is critical, such as moving flour from storage to packaging or transporting rice from processing stages to storage silos. However, these systems may require higher energy consumption and more complex maintenance compared to other options. HeadPowder’s pneumatic conveying equipment is built with corrosion-resistant materials and advanced control systems to ensure long-term reliability. The company’s solutions can handle materials with moisture content up to 15% and particle sizes as fine as 0.1 mm, making them versatile for various flour and rice processing needs.
3. Belt Conveyors: Versatile for Heavy and Bulk Loads
Belt conveyors are robust and versatile systems suitable for transporting heavy loads of rice and flour, including bulk bags or large sacks. These conveyors consist of a continuous belt that moves over rollers or idlers, carrying the material from one point to another. HeadPowder manufactures belt conveyors with heavy-duty belts and reinforced frames to handle high-capacity loads and harsh operating conditions. The company’s belt conveyor systems are available in various configurations, including inclined, horizontal, and curved designs, making them adaptable to different plant layouts. Key benefits of belt conveyors include their high load capacity (capable of handling up to 100 tons per hour), low maintenance costs, and ability to transport materials over long distances with minimal speed loss. They are ideal for applications like moving large quantities of rice from storage to processing facilities or conveying finished flour products to distribution centers. However, belt conveyors require more space and may need regular cleaning to prevent material buildup on the belt surface. HeadPowder’s belt conveyors are equipped with automatic cleaning systems and durable rubber belts to extend service life. The company’s designs can handle abrasive materials like milled flour and raw rice, ensuring consistent performance in demanding environments.
4. Bucket Elevators: Vertical Transport for High-Volume Operations
Bucket elevators are specialized vertical conveying systems designed for high-volume transport of rice and flour. These systems use a series of buckets attached to a chain or belt that moves vertically, lifting material from lower to upper levels. HeadPowder’s bucket elevators are engineered with durable buckets and robust drive mechanisms to handle continuous operation in industrial environments. The company’s vertical conveyors are available in various designs, such as chain bucket elevators or belt bucket elevators, to suit different material characteristics and processing requirements. Key advantages of bucket elevators include their high capacity (capable of transporting up to 200 tons per hour), vertical transport capability, and ability to handle materials with high moisture content or abrasive properties. They are commonly used in applications where vertical space is limited, such as moving rice from ground-level storage to upper-level processing equipment or conveying flour from grinding mills to storage silos. However, bucket elevators may require more maintenance and have higher initial costs compared to other horizontal conveying systems. HeadPowder’s bucket elevators feature anti-corrosion coatings and overload protection to ensure safety. The company’s designs are optimized for low noise operation and energy efficiency, making them suitable for continuous 24/7 operation in rice and flour processing plants.
5. Comparison Summary: Choosing the Right Conveying Method
When selecting a conveying method for rice and flour, several factors must be considered, including material characteristics, distance of transport, required capacity, and operational environment. Screw conveyors are ideal for short horizontal or vertical transport of bulk materials, while pneumatic systems excel in handling dusty or light materials over longer distances. Belt conveyors are suitable for heavy loads and large-scale operations, and bucket elevators are preferred for high-volume vertical transport. HeadPowder, with its expertise in industrial conveying equipment, offers a comprehensive range of solutions tailored to meet the specific needs of rice and flour processing plants. By understanding the advantages and limitations of each method, processors can make informed decisions to optimize their operations, improve efficiency, and ensure product quality. Whether you need to transport raw rice, milled flour, or other grain products, HeadPowder’s conveying systems provide reliable and efficient solutions for your industrial requirements. The company’s commitment to quality and customer satisfaction ensures that each conveying system is designed to meet the unique challenges of rice and flour processing, delivering long-term performance and value.